Large Vacuum Cups for Industrial Handling

application/large-vacuum-cups, application/large-vacuum-cups, 
Inquiry
Inquiry

large vacuum cups

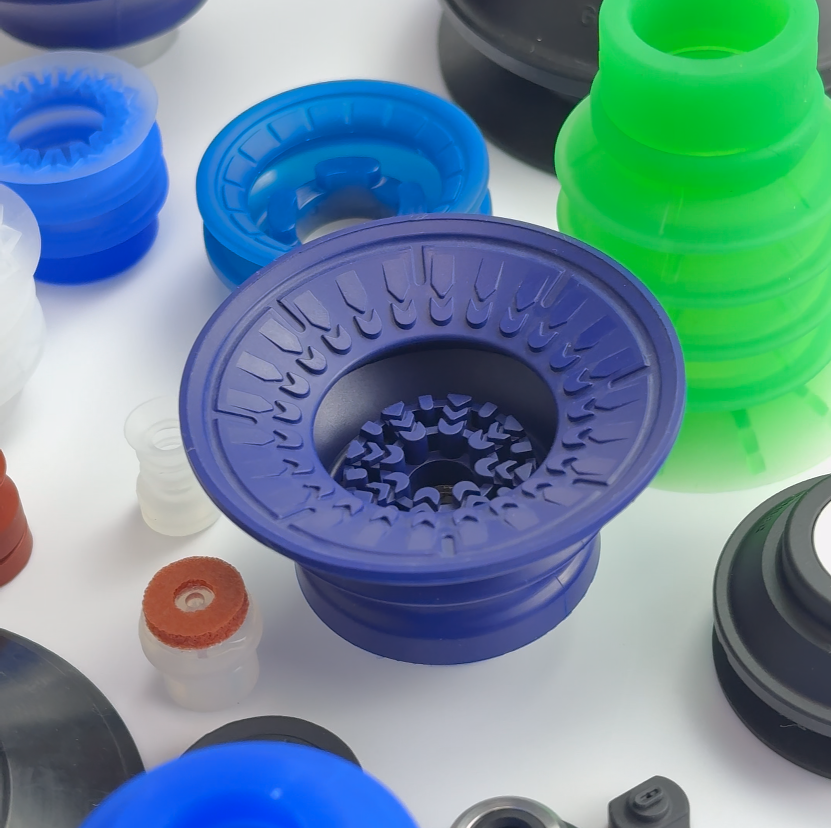
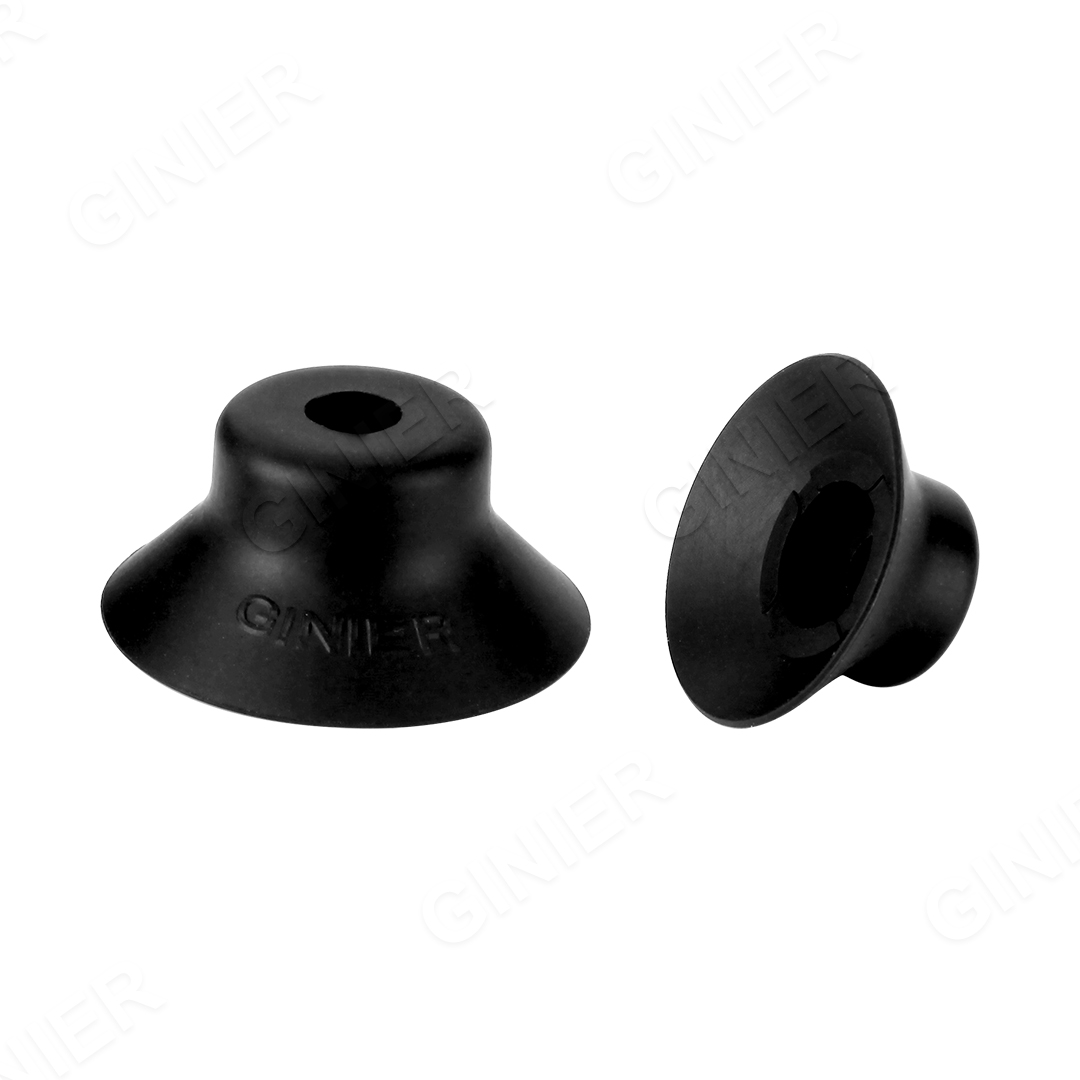
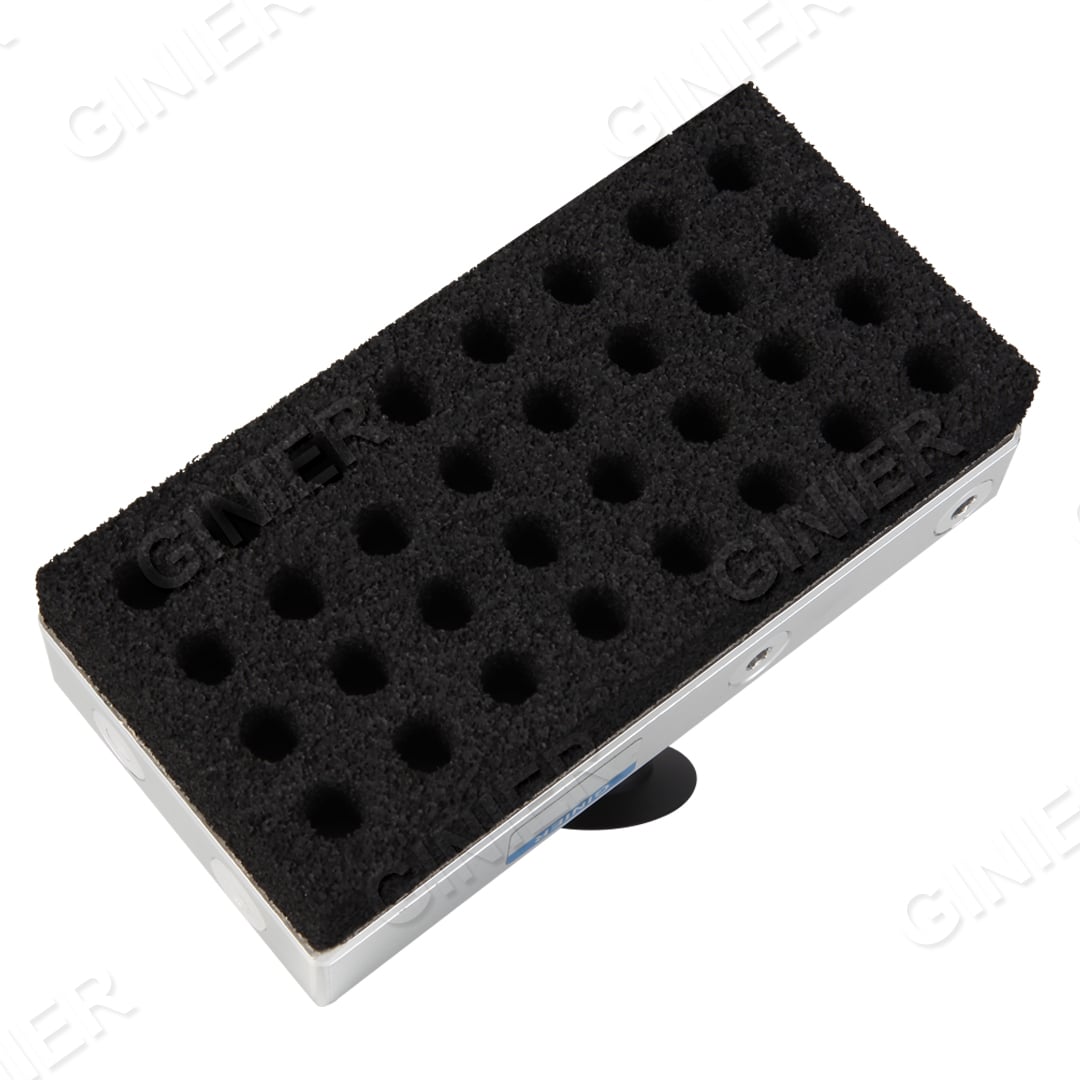
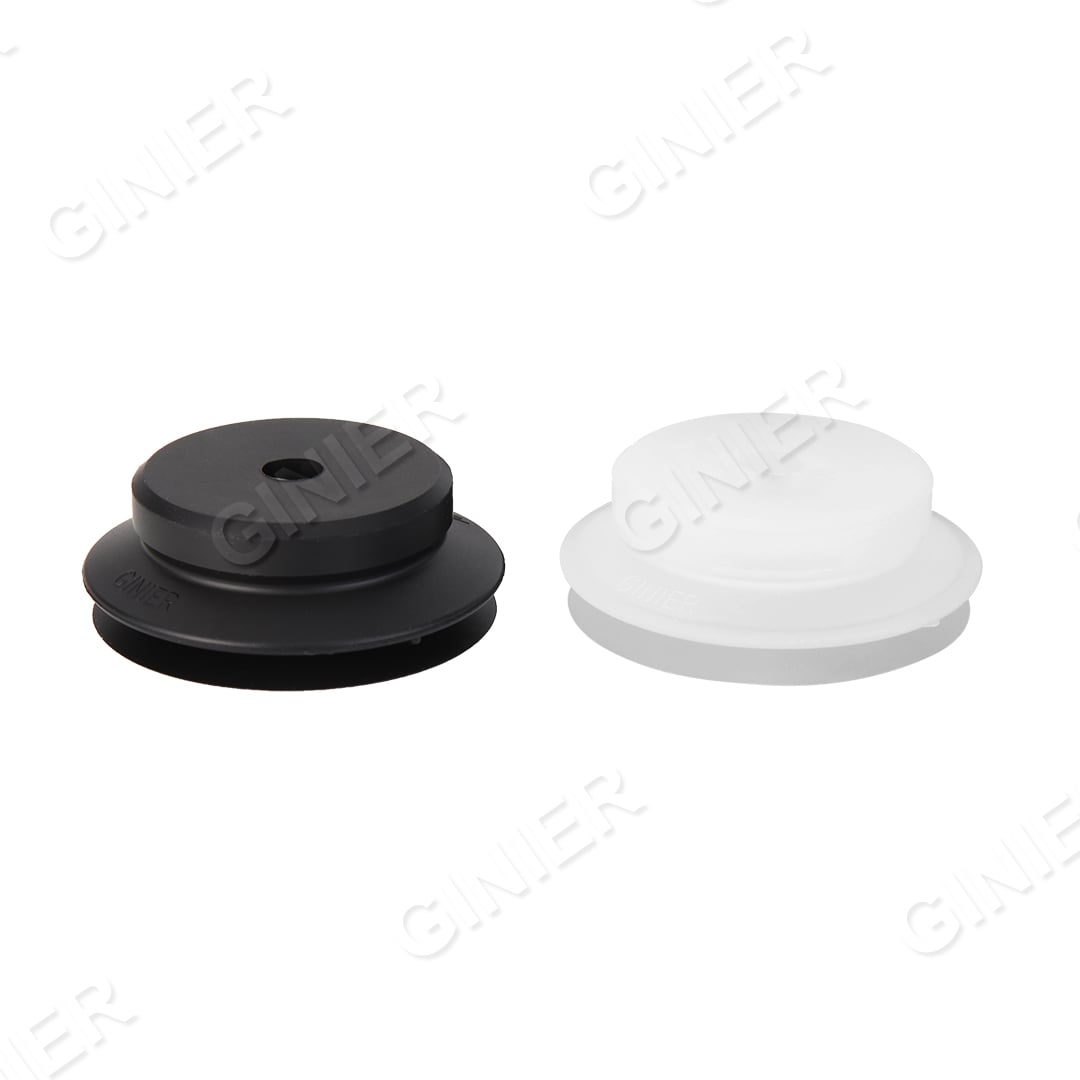
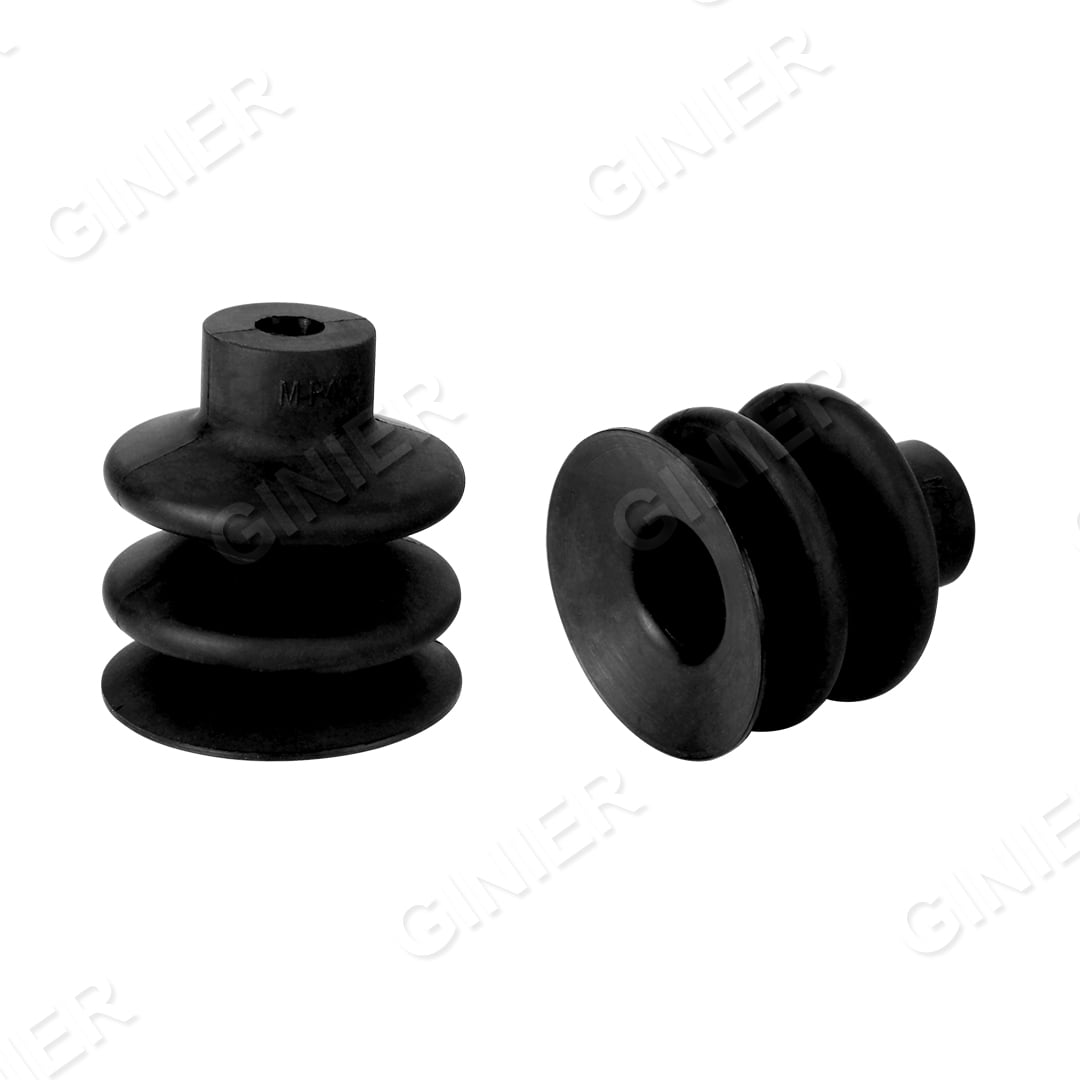
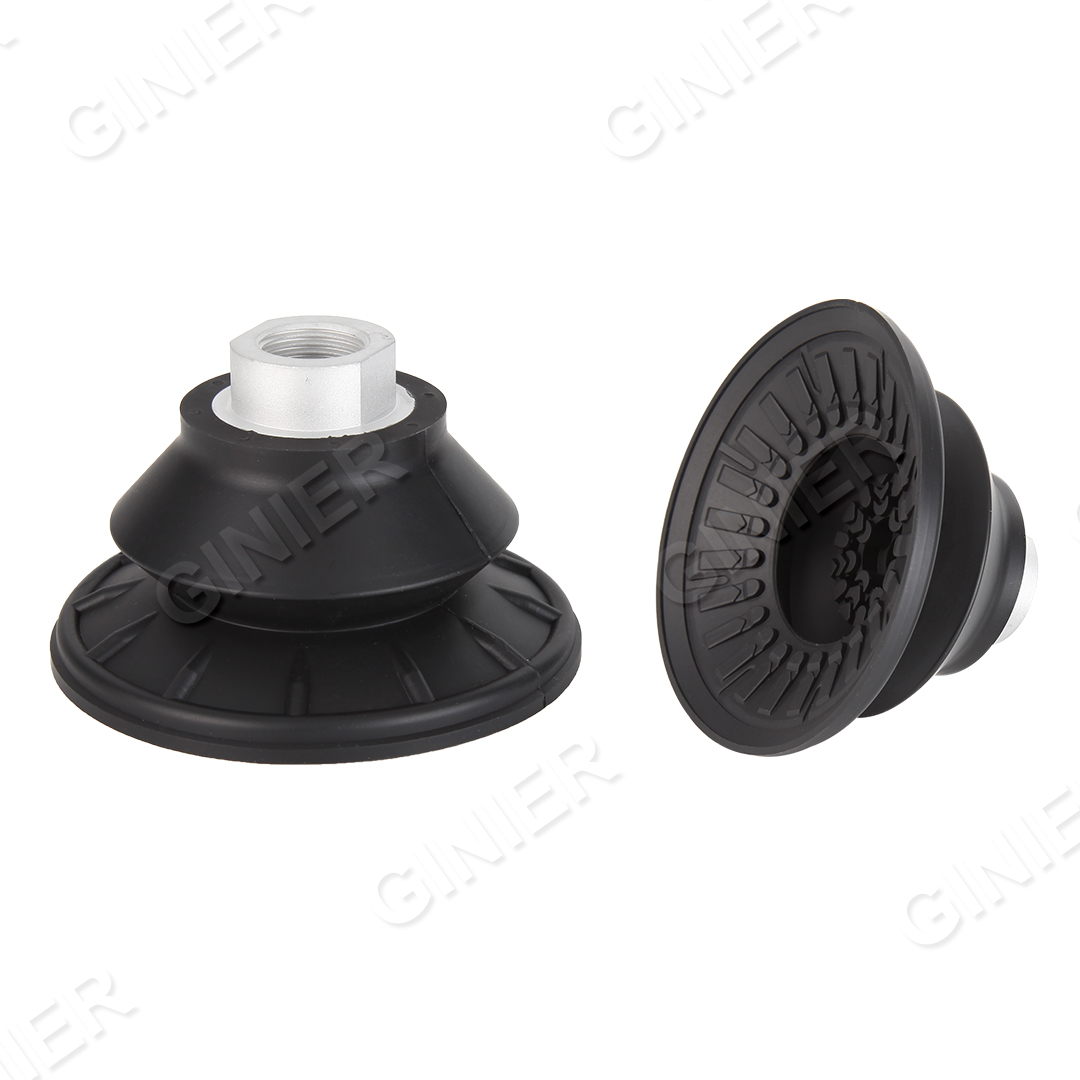
Large vacuum cups represent innovative lifting and holding solutions designed for industrial, manufacturing, and material handling applications. These specialized devices utilize advanced vacuum technology to create strong suction forces that securely grip objects of varying sizes, shapes, and materials. Large vacuum cups function by removing air between the cup surface and the object being lifted, generating negative pressure that holds items firmly in place without causing damage. The technological features of large vacuum cups include precision-engineered rubber or silicone materials that provide optimal grip and durability. Modern large vacuum cups incorporate multi-layer construction with reinforced walls that withstand repetitive use and maintain consistent performance. These cups feature valve systems that regulate air flow, ensuring controlled attachment and release cycles. Advanced designs include integrated sensors that monitor suction levels and detect potential failures before they occur. Applications for large vacuum cups span diverse industries including automotive manufacturing, glass handling, wood processing, and pharmaceutical production. These tools excel in automated systems where precision and reliability are critical requirements. Large vacuum cups handle delicate items like glass panels, mirrors, and electronic components with exceptional care. They accommodate heavy loads in warehouse automation and facilitate efficient material transfer in production environments. The versatility of large vacuum cups makes them indispensable in modern industrial operations seeking improved efficiency and worker safety.
Large vacuum cups deliver substantial operational benefits that transform material handling efficiency across industries. The primary advantage centers on safety enhancement, as these cups eliminate manual lifting risks and reduce workplace injuries significantly. Workers can transport heavy, awkward items safely using large vacuum cups, protecting their health while maintaining productivity levels. Operational benefits include remarkable speed improvements in material transfer processes. Large vacuum cups enable faster handling cycles compared to traditional mechanical gripping methods, directly reducing production time and increasing output capacity. These solutions integrate seamlessly into automated systems, creating synchronized workflows that maximize throughput without requiring extensive equipment modifications. The practical value for business operations manifests through cost reduction and resource optimization. Large vacuum cups minimize product damage during handling, decreasing waste and improving profitability. Their durability ensures extended service life, lowering replacement frequency and maintenance expenses. Facilities using large vacuum cups experience reduced labor costs since fewer personnel handle physically demanding tasks. Application suitability represents another decisive advantage, as large vacuum cups adapt to multiple surfaces and materials. Whether handling glass, plastics, metals, or composites, these cups provide reliable performance across diverse conditions. The customizable design options mean businesses select large vacuum cups specifically engineered for their unique operational requirements. Decision-useful context highlights that large vacuum cups represent smart investments for companies modernizing their material handling infrastructure. Organizations prioritizing worker safety, productivity enhancement, and cost efficiency find large vacuum cups deliver measurable returns on investment while supporting sustainable business growth and operational excellence.

Practical Tips

Meet GINIER | 2026 South China International Industry Fair

04

Aug

Meet GINIER | 2026 South China International Industry Fair

View More
GINIER Wishes All Workers a Happy Labour Day

04

Aug

GINIER Wishes All Workers a Happy Labour Day

View More
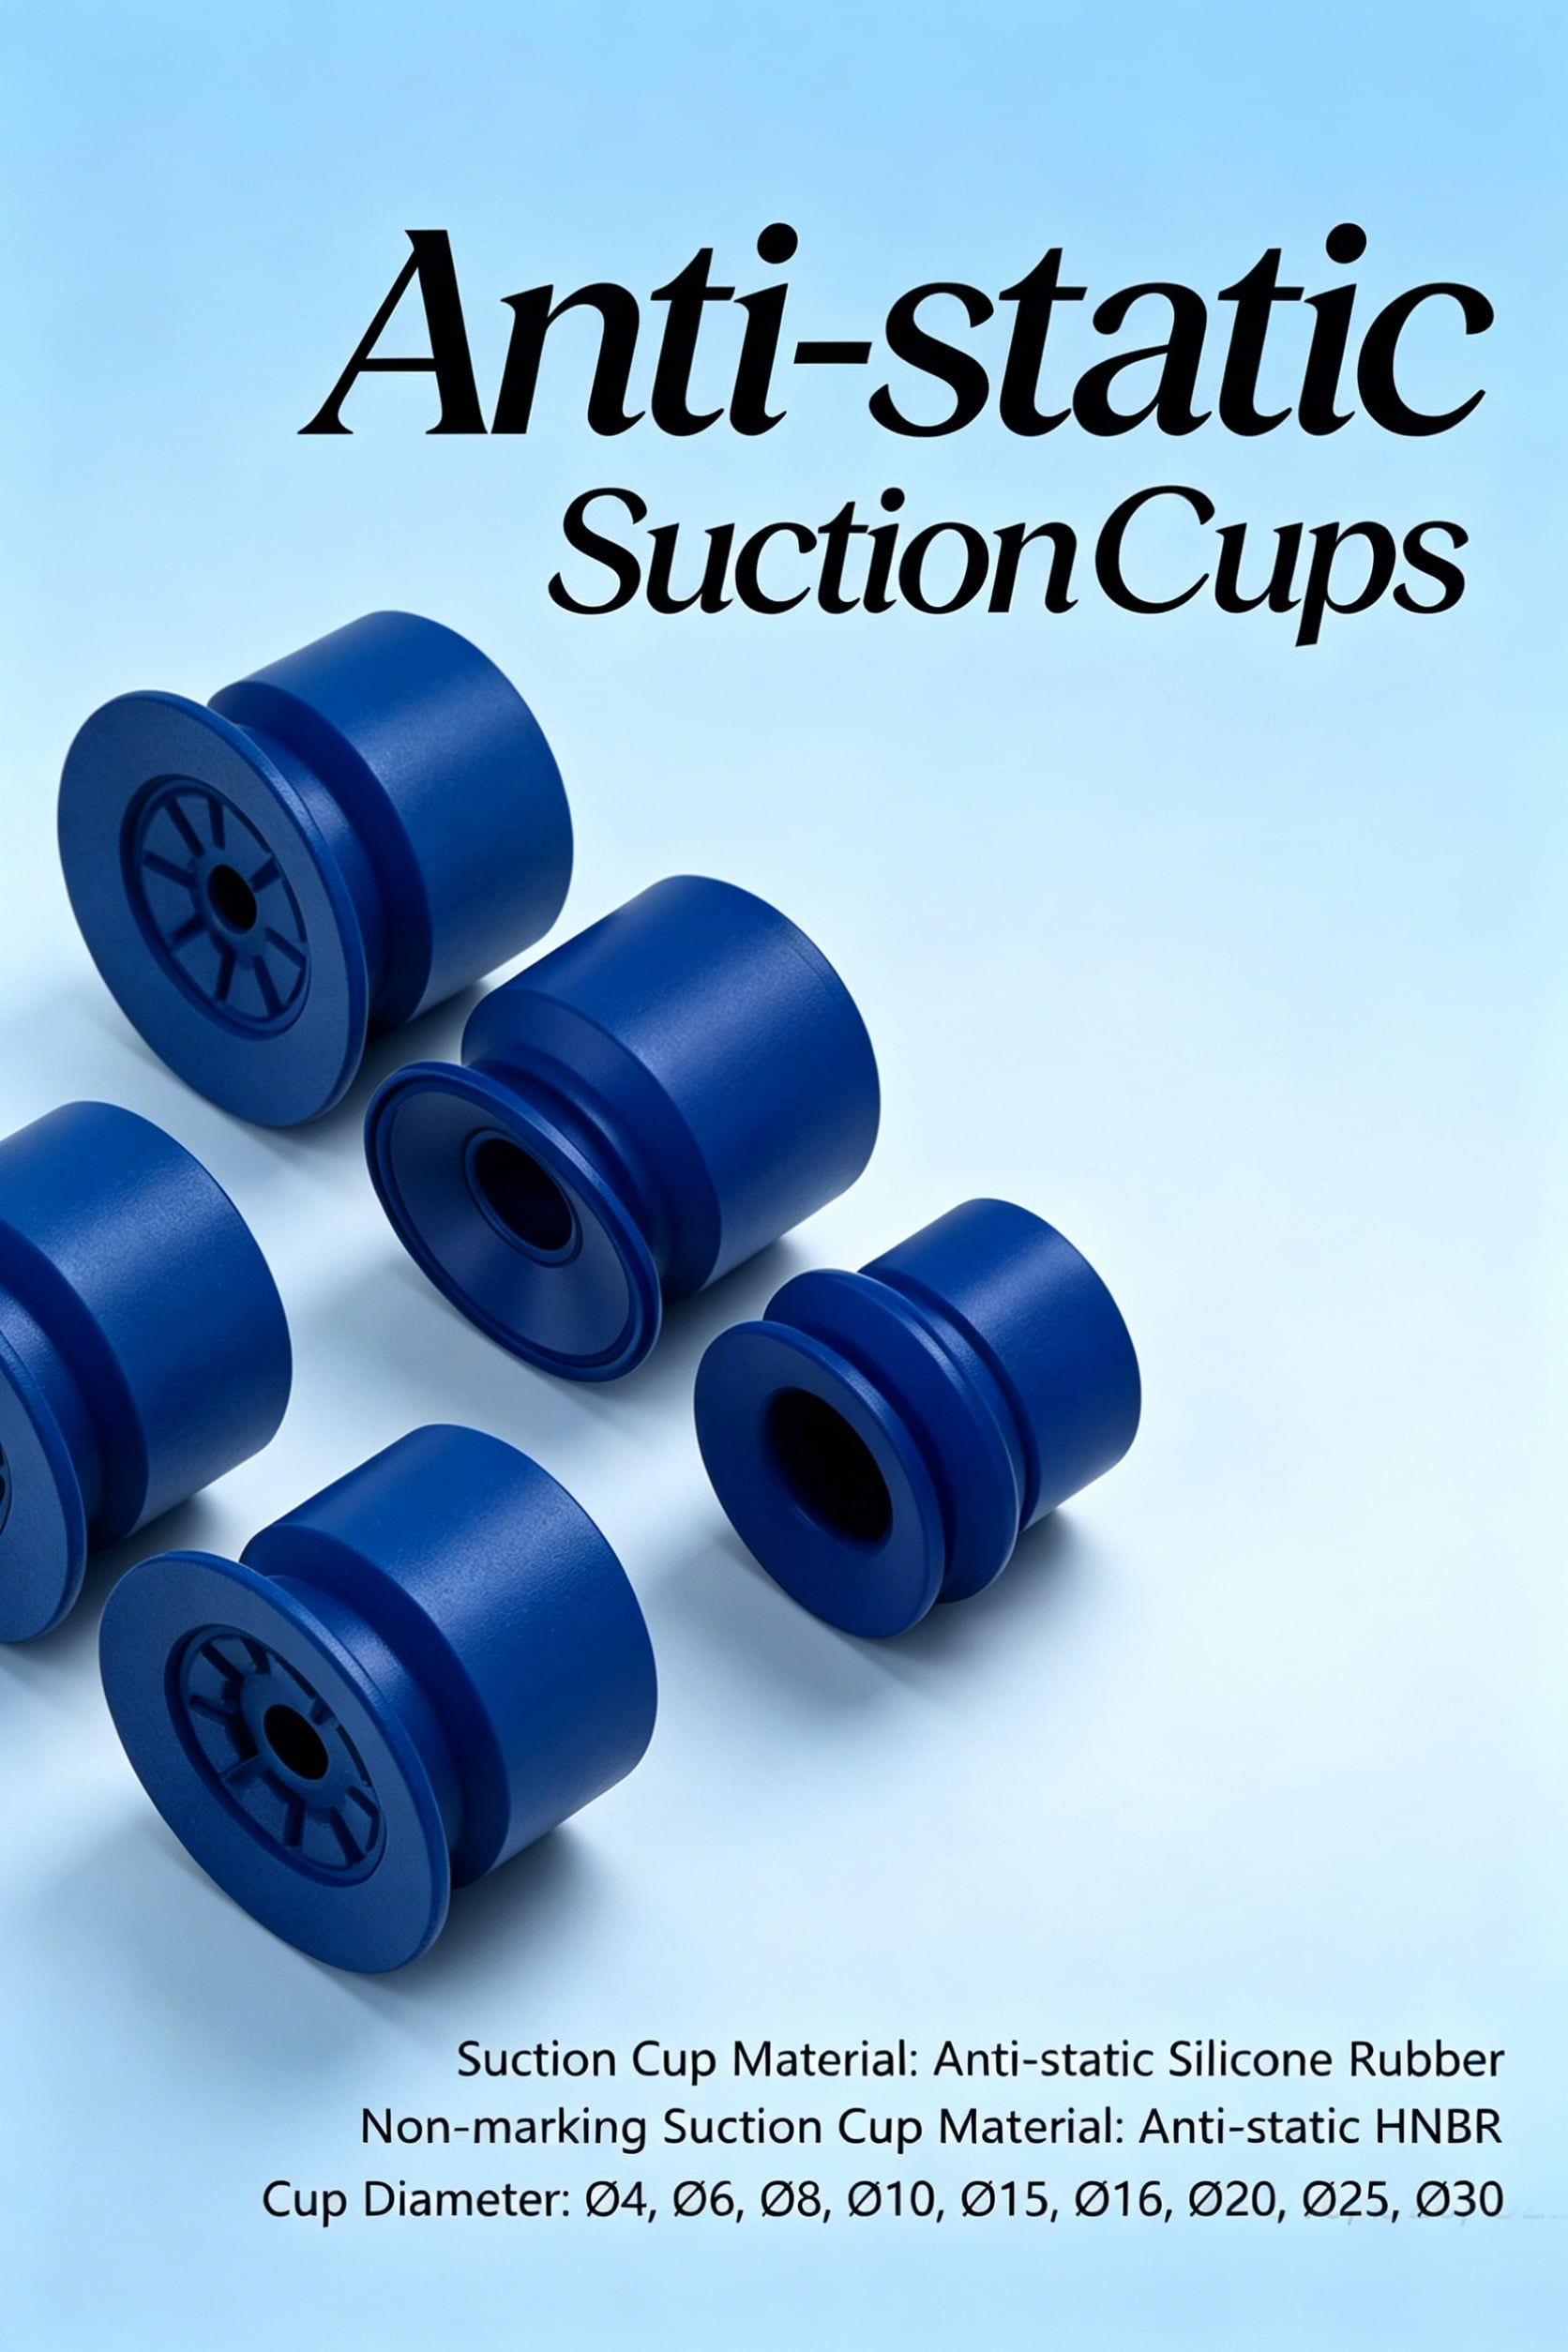
GINIER New HBUE Anti-static Suction Cups Launched

04

Aug

GINIER New HBUE Anti-static Suction Cups Launched

View More

Superior Suction Power and Reliable Performance

Superior Suction Power and Reliable Performance

Large vacuum cups demonstrate exceptional suction capabilities that securely hold items weighing up to several hundred pounds depending on specifications and surface conditions. The engineering precision in large vacuum cups creates consistent negative pressure that remains stable throughout material transfer operations. Advanced valve technology integrated into modern large vacuum cups automatically compensates for minor pressure fluctuations, maintaining steadfast grip even during movement or vibration. This reliability eliminates costly product drops and workplace accidents that damage both materials and company reputation. Users trust large vacuum cups for handling their most valuable items because the superior suction power ensures predictable, dependable performance across varying industrial applications. Whether processing delicate glass components or heavy metal parts, large vacuum cups deliver the powerful, consistent hold required for safe, efficient operations.
Durable Construction for Extended Service Life

Durable Construction for Extended Service Life

Large vacuum cups feature robust materials engineered to withstand intensive industrial environments and frequent use cycles. The reinforced silicone and rubber components in quality large vacuum cups resist degradation from oils, chemicals, and temperature extremes that typically reduce equipment lifespan. Manufacturers design large vacuum cups with multi-layer construction that prevents premature wear, extending operational life significantly beyond standard alternatives. This durability translates directly to reduced maintenance requirements and lower total cost of ownership for businesses. Organizations investing in premium large vacuum cups experience fewer unexpected failures and emergency replacements that disrupt production schedules. The resilient construction ensures large vacuum cups maintain consistent performance quality throughout their extended service period, protecting business operations and maximizing investment returns.
Versatile Applications Across Multiple Industries

Versatile Applications Across Multiple Industries

Large vacuum cups adapt remarkably well to diverse material handling scenarios across automotive, electronics, glass, pharmaceutical, and food processing sectors. The customizable design options available for large vacuum cups accommodate different surface types, from smooth glass to textured composites and metal surfaces. Industries worldwide specify large vacuum cups for specialized applications requiring precision, care, and reliability that standard handling methods cannot provide. From automated assembly lines to warehouse distribution centers, large vacuum cups solve complex handling challenges efficiently. Manufacturers develop specialized variations of large vacuum cups addressing industry-specific requirements, ensuring businesses access solutions tailored perfectly to their operational needs and production parameters.